About 100 LPH Reverse Osmosis Water Purifier
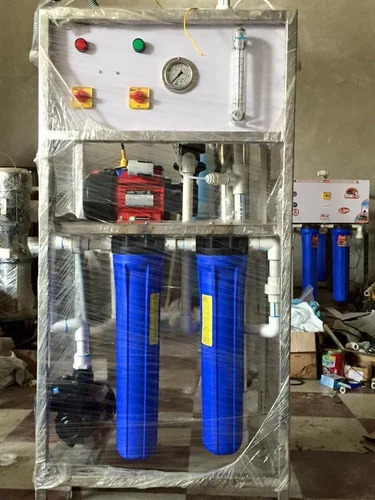
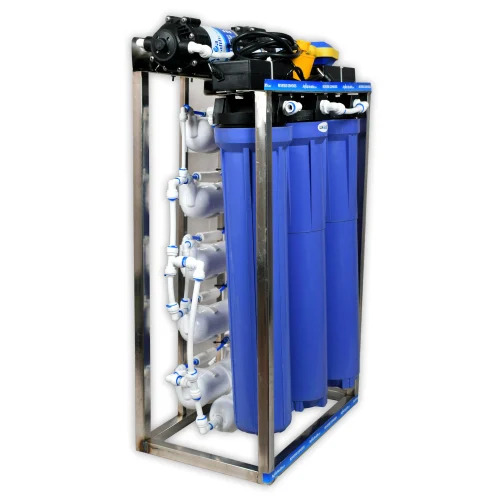
Unlock the power of peerless industrial water purification with our 100 LPH Reverse Osmosis Water Purifier. Fresh innovation meets first-rate technology, featuring select TFC membranes and unparalleled double blue pre-filtration housings. The compact, floor-standing design-crafted with sturdy stainless steel support-ensures seamless operation in limited spaces. Equipped with an analog control panel and integrated pressure gauges, this semi-automatic RO purifier guarantees unprecedented reliability and consistency. Suitable for bore water, it delivers a consistent 100 liters per hour, ideal for industrial applications demanding pure, contaminant-free water. Installation and essential accessories included for immediate productivity.
Industrial Performance and Application
The 100 LPH Reverse Osmosis Water Purifier is designed for industrial water purification, serving manufacturers, service providers, traders, and suppliers across various sectors. Used primarily for treating bore water, it is perfect for laboratories, factories, and other high-demand settings. The distinct advantage lies in its high flow rate and absence of inbuilt storage, ensuring continual, on-demand purification. Its heavy-duty construction promises durability, while its semi-automatic features provide operational efficiency without complexity.
Certifications, Export Markets, and Payment Options
Certified under stringent quality standards for industrial RO systems, this purifier is actively exported to major markets across Asia and the Middle East. We offer competitive asking prices and list prices, tailored for bulk supply and long-term contracts. Express shipping is available for urgent requirements, and payment terms are transparent and flexible, including advance payments and net term arrangements via trusted banking channels. Global support ensures you receive top-tier service wherever your business operates.
FAQ's of 100 LPH Reverse Osmosis Water Purifier:
Q: How is the 100 LPH Reverse Osmosis Water Purifier installed at a site?
A: Our product includes an expert installation service. The compact floor-standing purifier is set up by our trained technicians, who also connect piping, fittings, and filters for seamless operation.
Q: What are the main benefits of using a semi-automatic RO water purifier for industrial purposes?
A: A semi-automatic RO system offers operational control, reliability, and efficient purification, reducing downtime and ensuring continuous delivery of clean water suited for intricate industrial processes.
Q: What water sources are compatible with this purifier?
A: The unit is designed specifically for bore water but can also handle various other industrial water sources, provided the feedwater meets the system's pre-filtration requirements.
Q: Where can this 100 LPH RO purifier be most effectively used?
A: This model is perfect for industrial locations such as manufacturing plants, research laboratories, warehouses, and other high-usage environments demanding uninterrupted water purification.
Q: What process does the 100 LPH RO water purifier use?
A: It utilizes advanced Thin-Film Composite (TFC) reverse osmosis membranes, along with double blue pre-filters and a heavy-duty pump, to deliver high-flow, contaminant-free water.




 Send Inquiry


 Send Inquiry
 Send Inquiry
