About Industrial Reverse Osmosis Plant
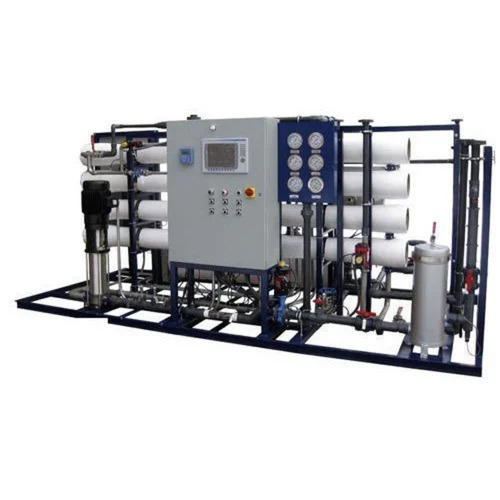
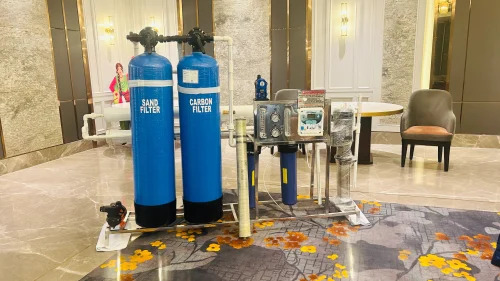
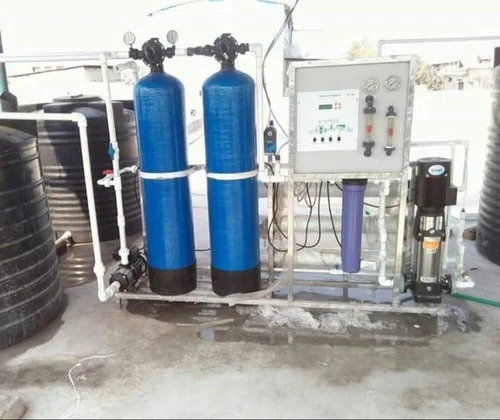
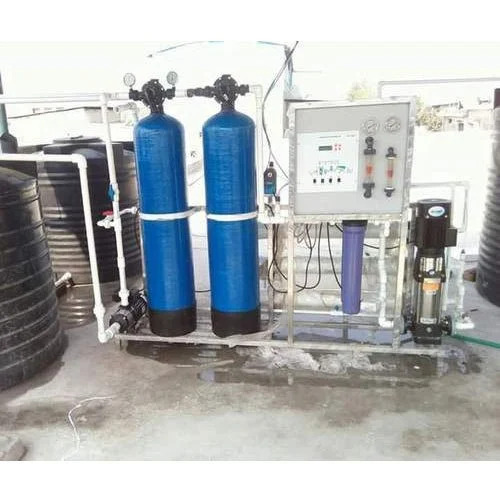
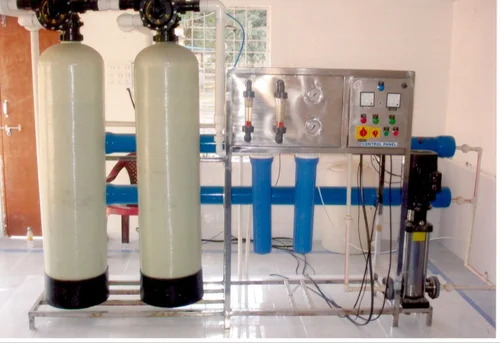
Unlock premier water purity with our Industrial Reverse Osmosis Plant-a sensational hot deal for manufacturers, service providers, suppliers, and traders in India. This potent, highly recommended unit features a powder-coated metal frame and modular skid suitable for robust floor mounting. Enjoy a special discount while benefiting from a digital control panel, automatic operation, and integrated pretreatment filters. The plant delivers a substantial 100 LPH capacity, built with durable FRP materials. Ideal for diverse industrial applications, this automatic-grade RO system guarantees efficiency and dependability for commercial water purification needs.
Industrial RO Plant: Advanced Features for Professionals
Our Industrial Reverse Osmosis Plant stands out with its digital control panel, modular skid design, powder-coated metal frame, and automatic operations. Widely used in commercial setups by manufacturers, service providers, suppliers, and traders, it efficiently purifies water for a broad range of industrial processes. The easy integration of pretreatment filters enhances filtration and system longevity. This premier solution is tailored to meet the demanding requirements of industrial environments, ensuring reliable water treatment with minimal intervention.
Prompt Delivery, Certifications & Global Markets
Enjoy quick dispatch and competitive sale prices when you order our Industrial Reverse Osmosis Plant. Each unit is dispatched with care, ensuring swift and safe transportation. It is certified for quality compliance and designed to meet international standards. We primarily export to Asian, Middle Eastern, and African markets, making this product a preferred choice for global industrial clients. Take advantage of our prompt service and certified quality to enhance your business operations efficiently.
FAQ's of Industrial Reverse Osmosis Plant:
Q: How does the Industrial Reverse Osmosis Plant operate automatically?
A: The plant integrates a digital display control panel and advanced sensors, allowing it to function automatically-monitoring water quality, adjusting settings, and ensuring consistent operation without manual intervention.
Q: What is the process of water filtration in this RO Plant?
A: Water passes through integrated pretreatment filters to remove large particulates and contaminants, followed by reverse osmosis membranes that eliminate dissolved impurities, producing purified water suitable for industrial use.
Q: Where can this Industrial RO Plant be installed?
A: This system is floor-mounted and suitable for any industrial setting, including factories, warehouses, and commercial water treatment facilities requiring reliable, large-scale water purification.
Q: What are the typical applications and commercial uses?
A: The RO plant is widely used for process water, boiler feed, cooling tower makeup, food and beverage manufacturing, pharmaceuticals, and any industrial application that demands high-quality purified water.
Q: When can I expect delivery after placing an order?
A: We ensure quick dispatch following confirmation, with units rapidly shipped to meet urgent needs. Delivery timelines depend on your location and specific order requirements, but prompt fulfillment is prioritized.
Q: What are the benefits of choosing this RO Plant over traditional filtration systems?
A: This advanced RO system delivers higher efficiency, superior contaminant removal, fully automatic operations, and a long service life thanks to its robust construction and integrated treatment features.




 Send Inquiry


 Send Inquiry
 Send Inquiry
